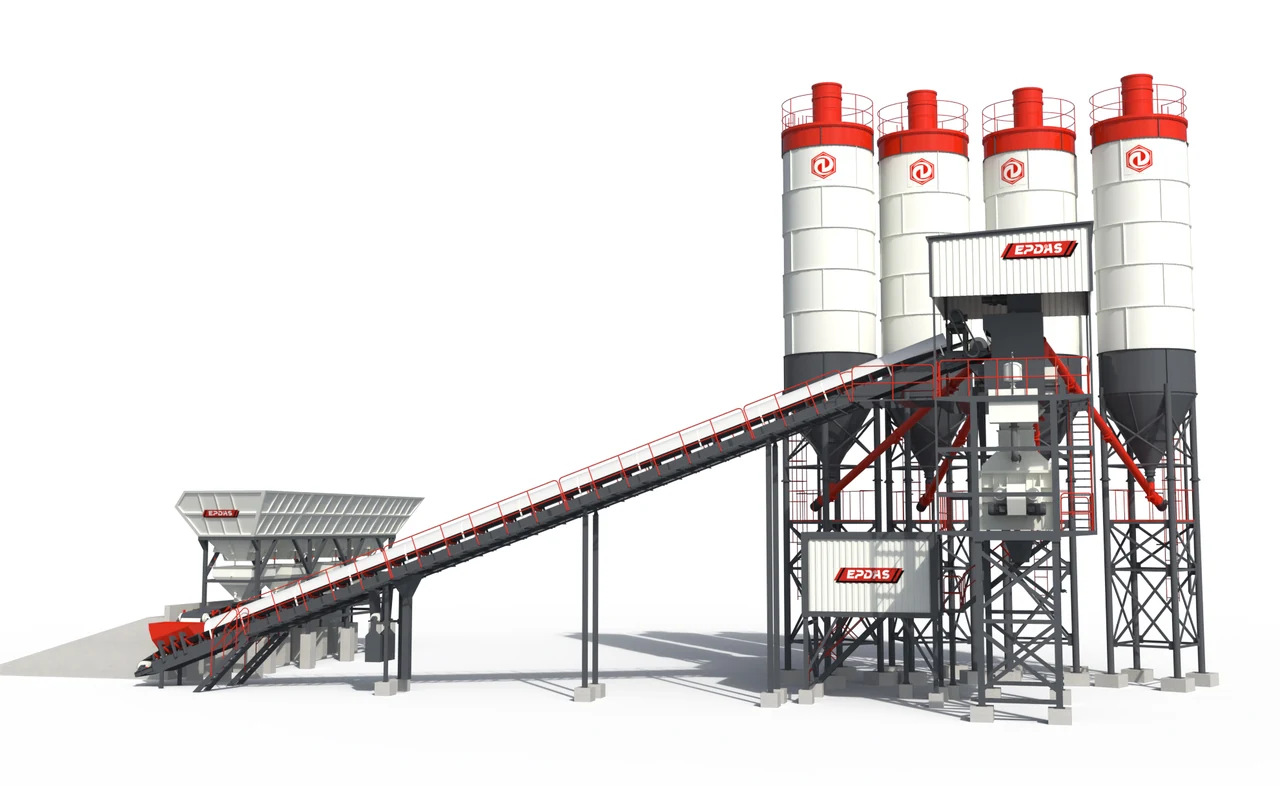
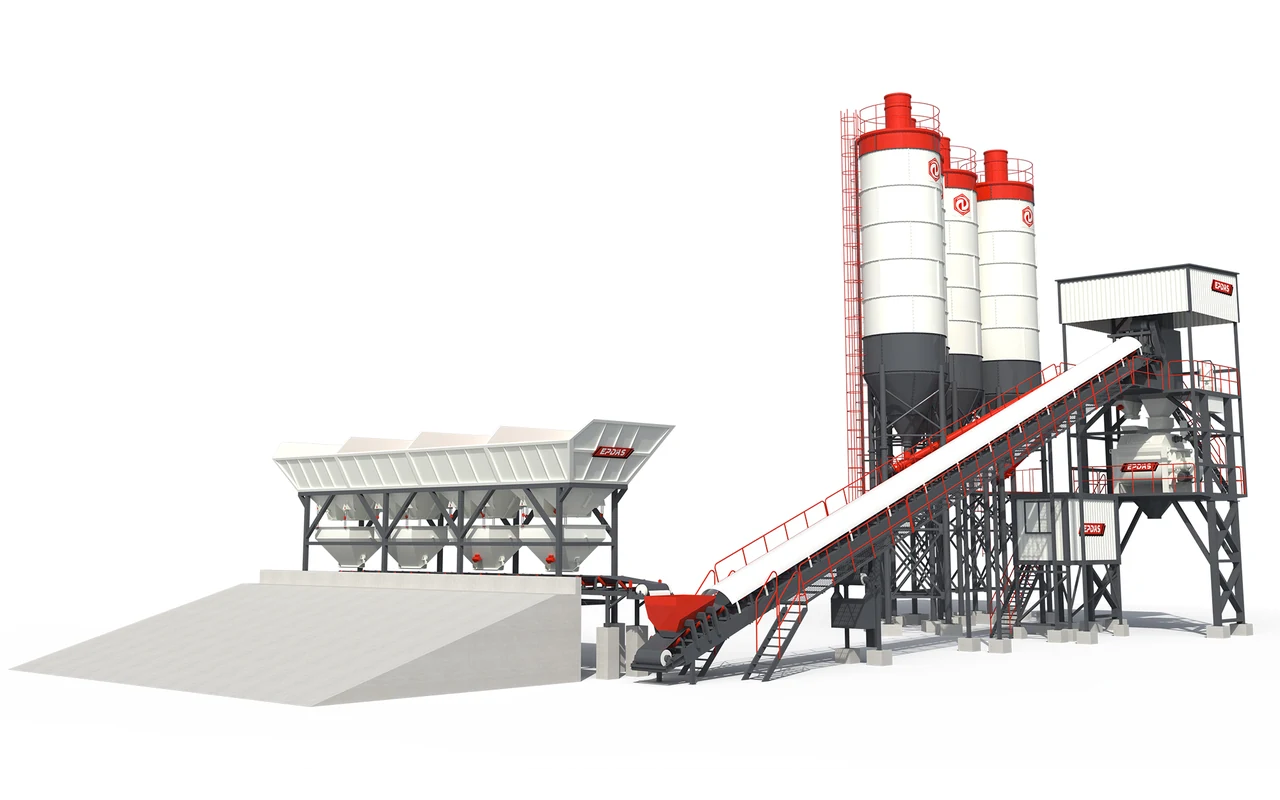
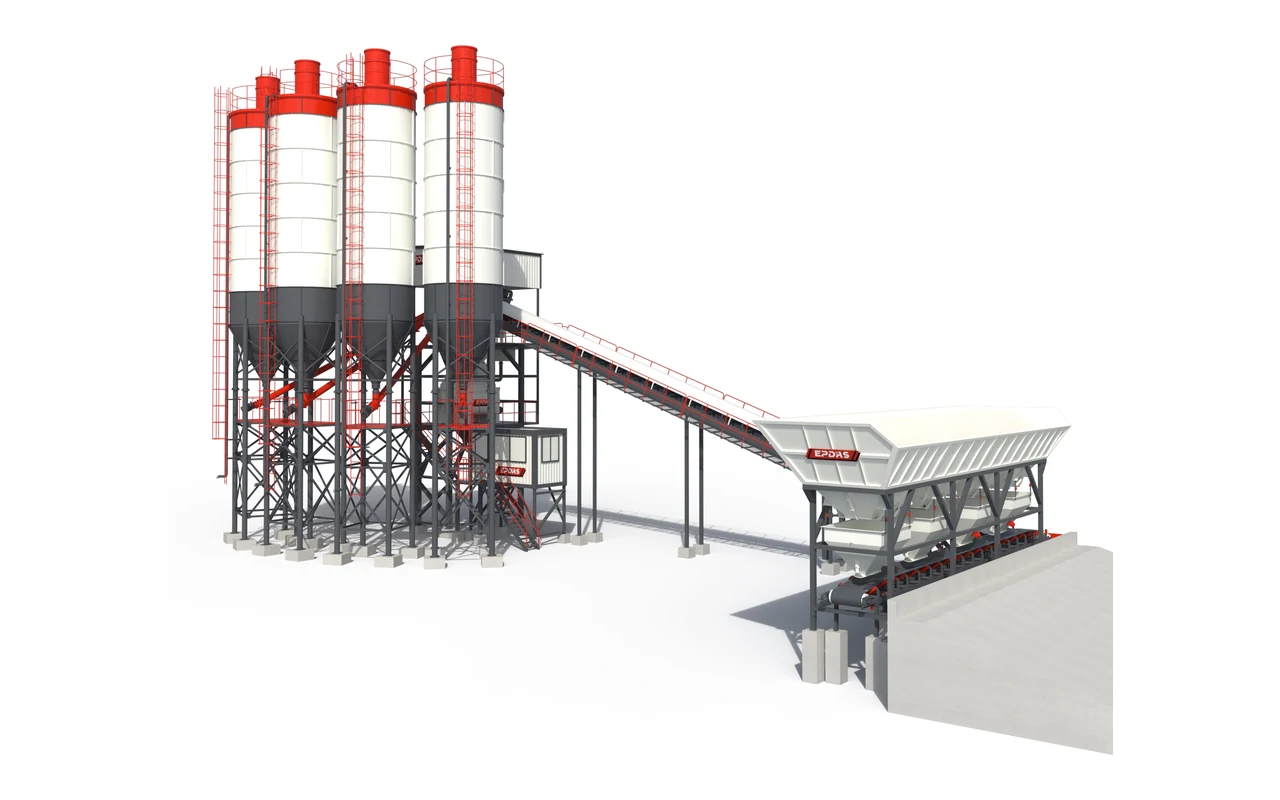
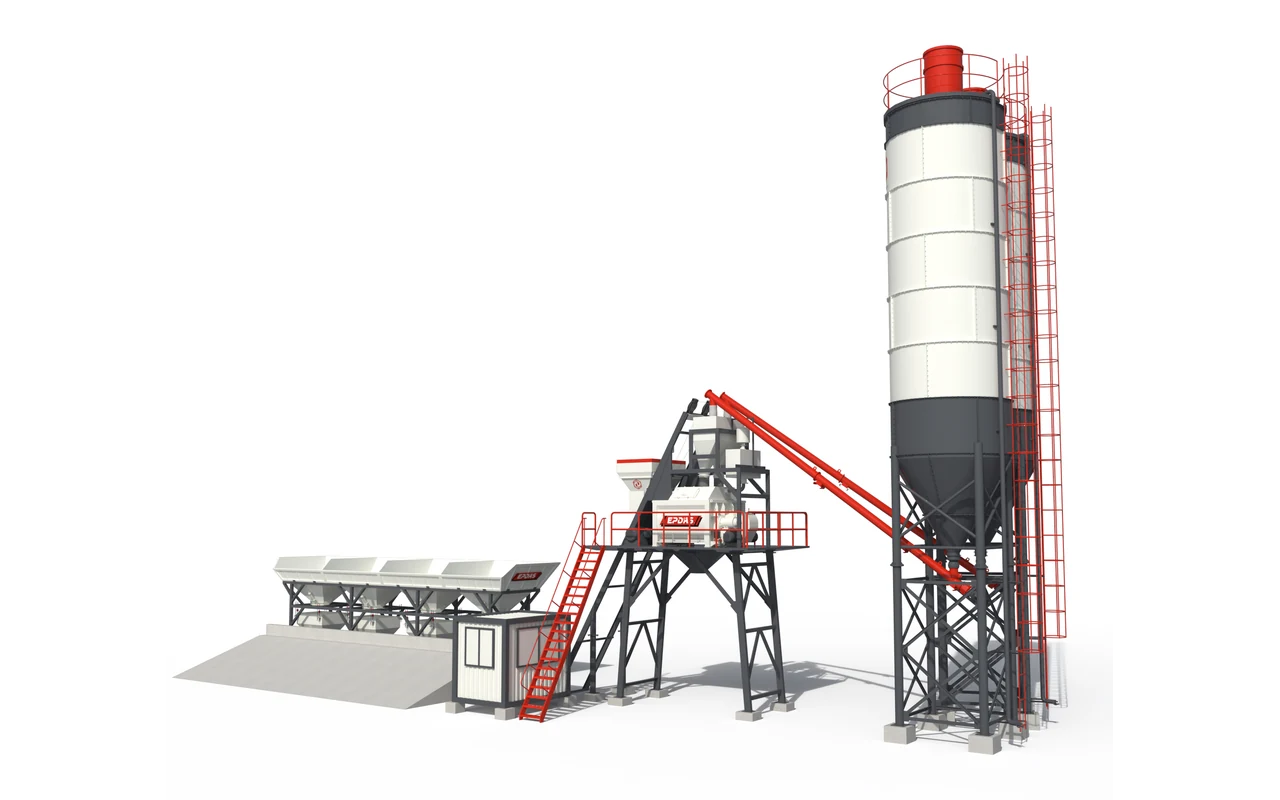
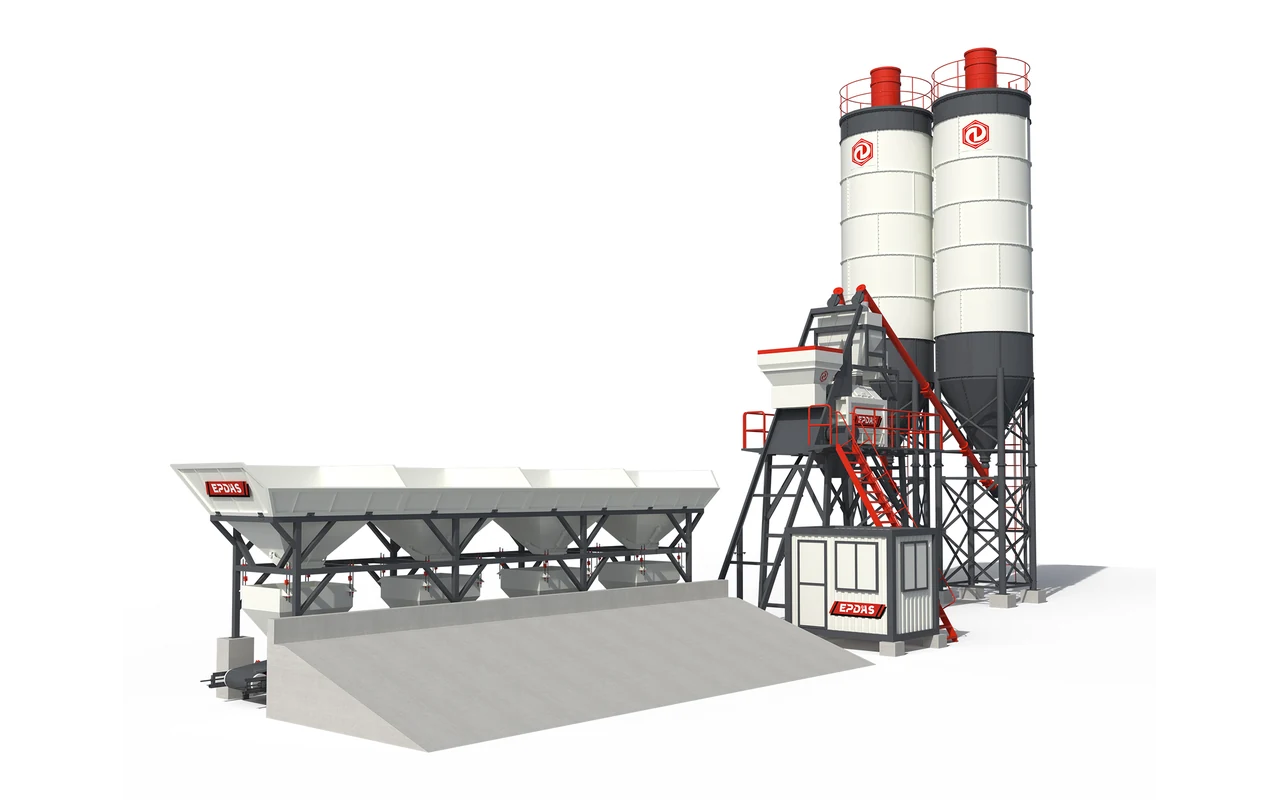
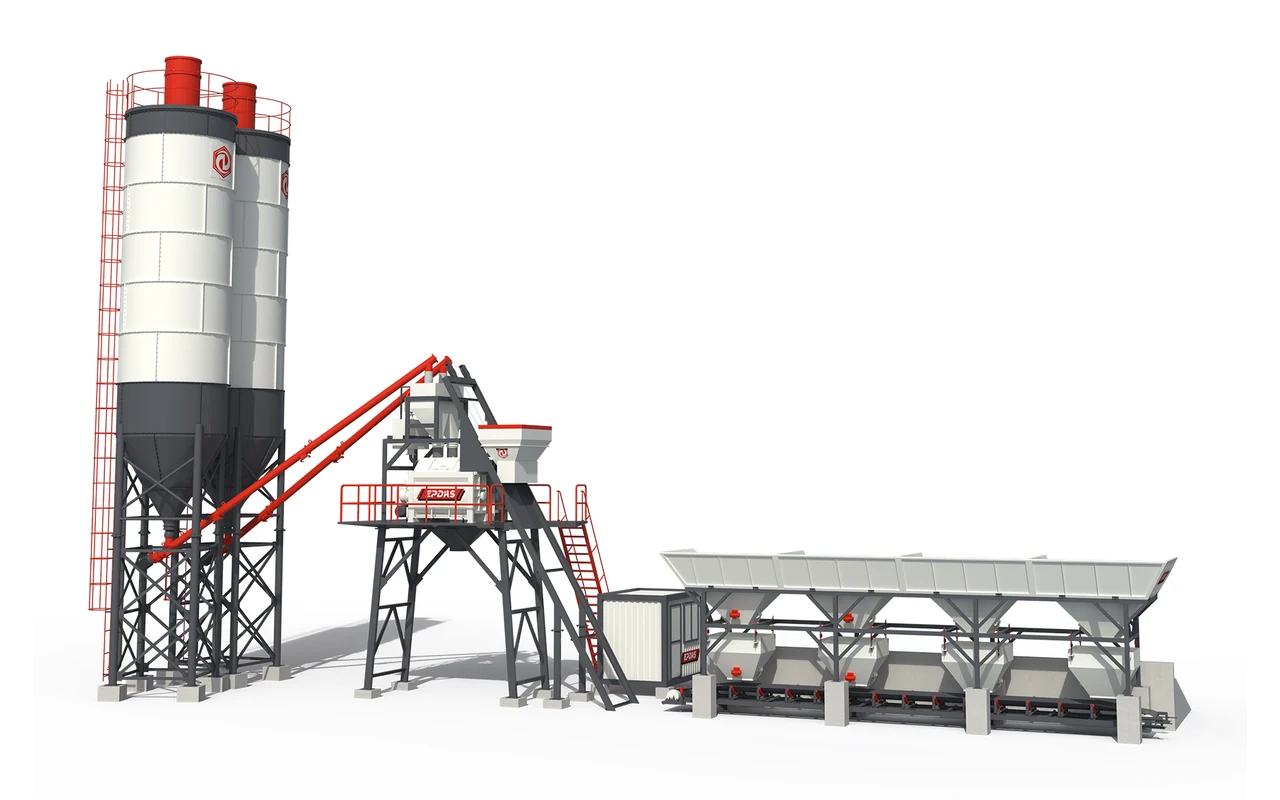
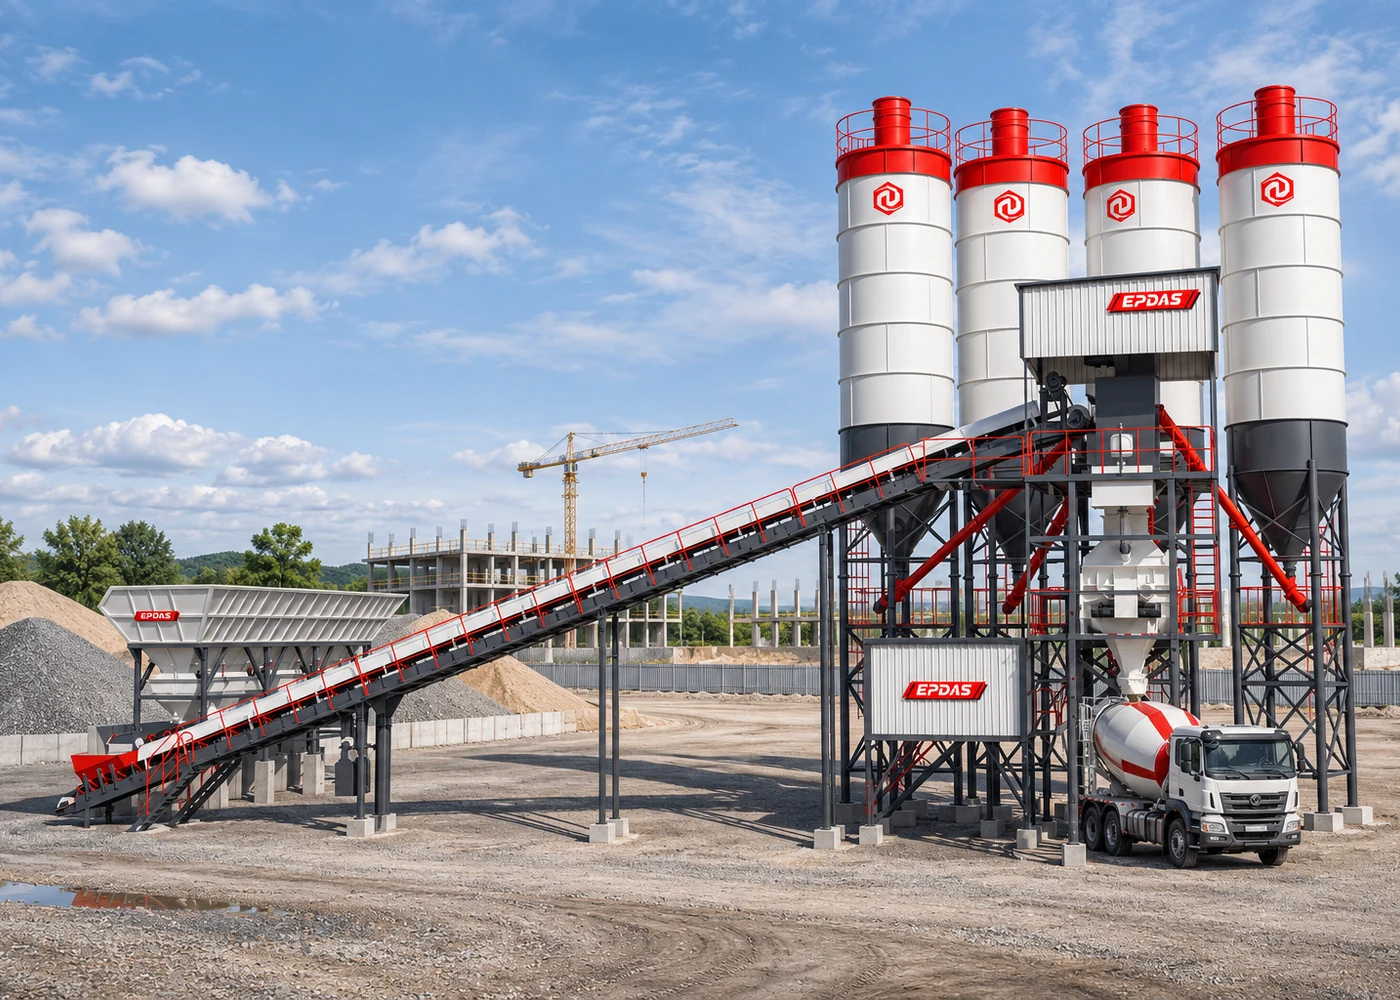
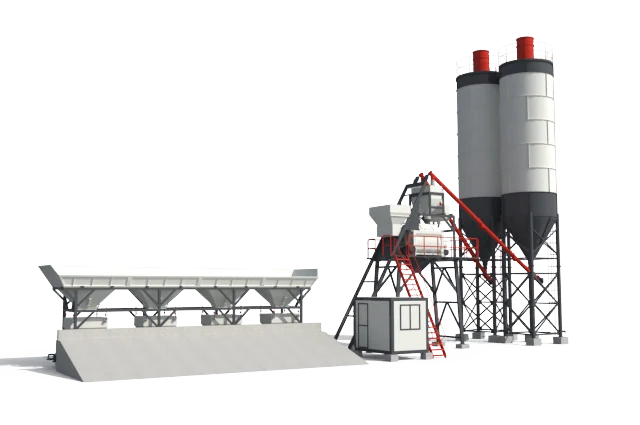
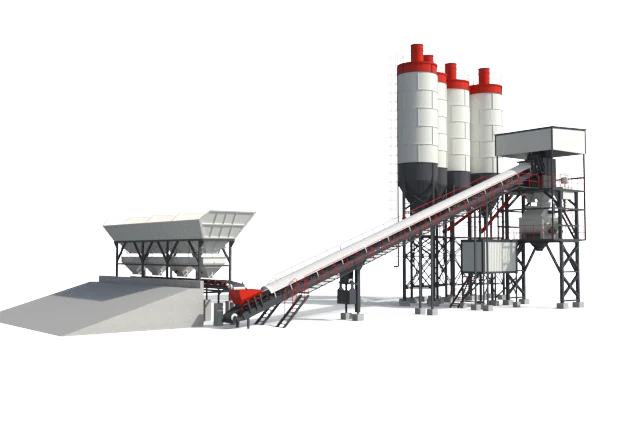
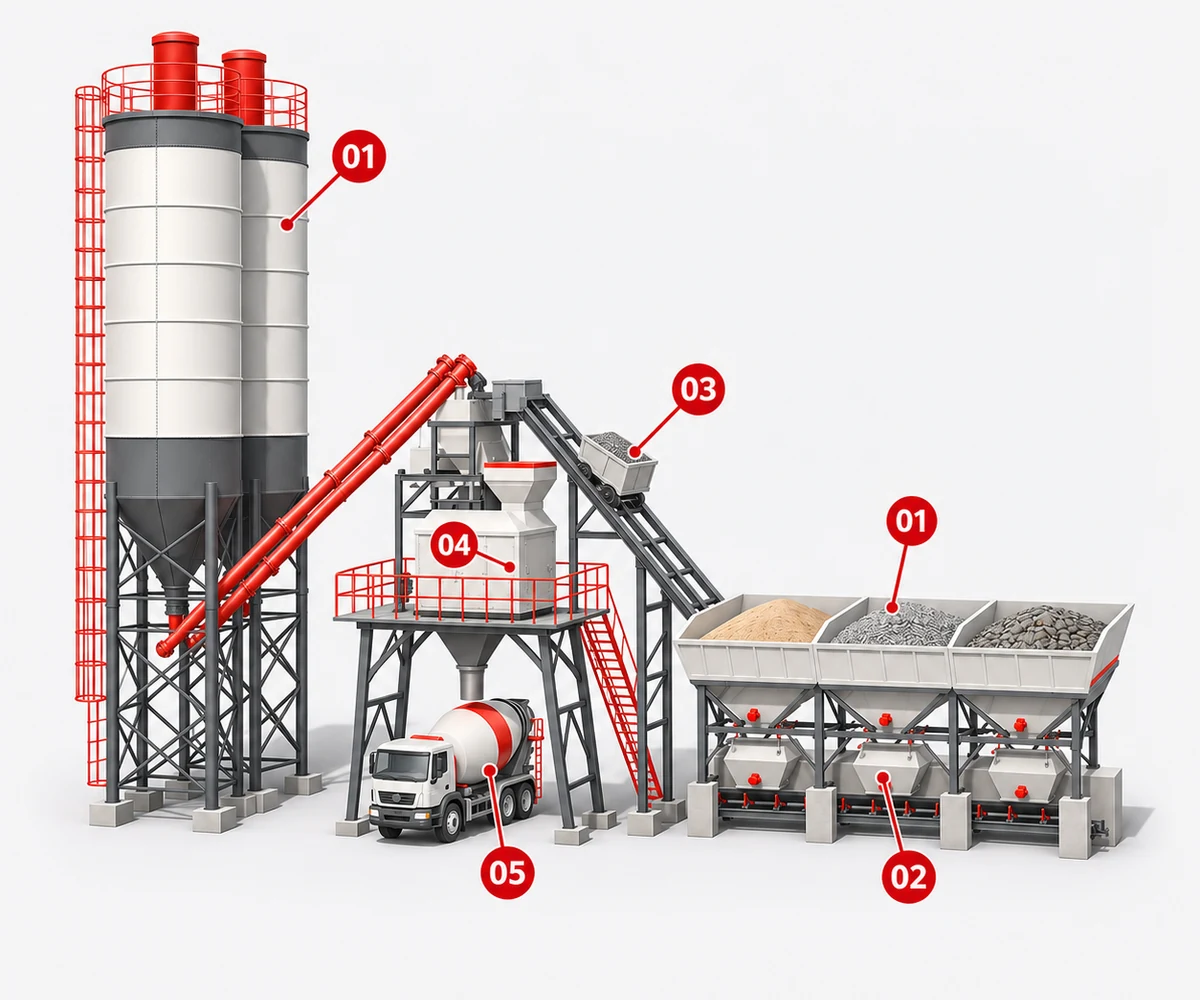
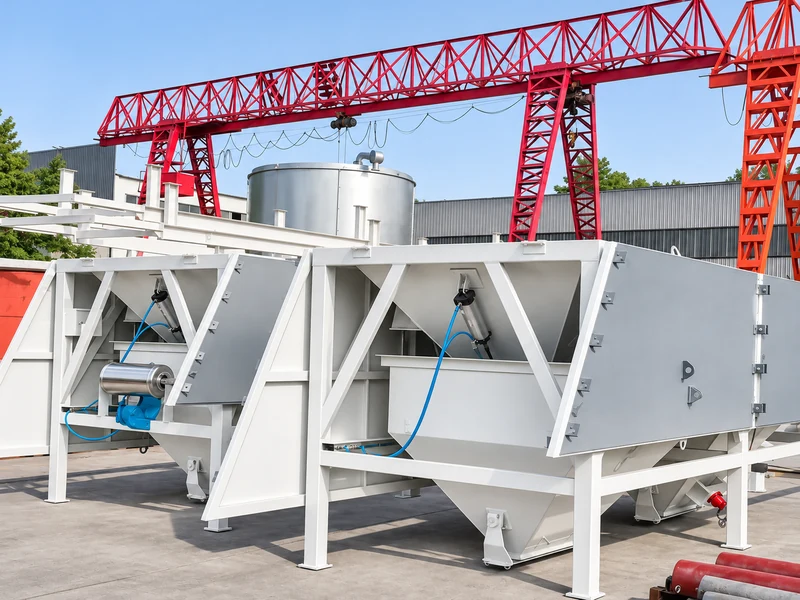
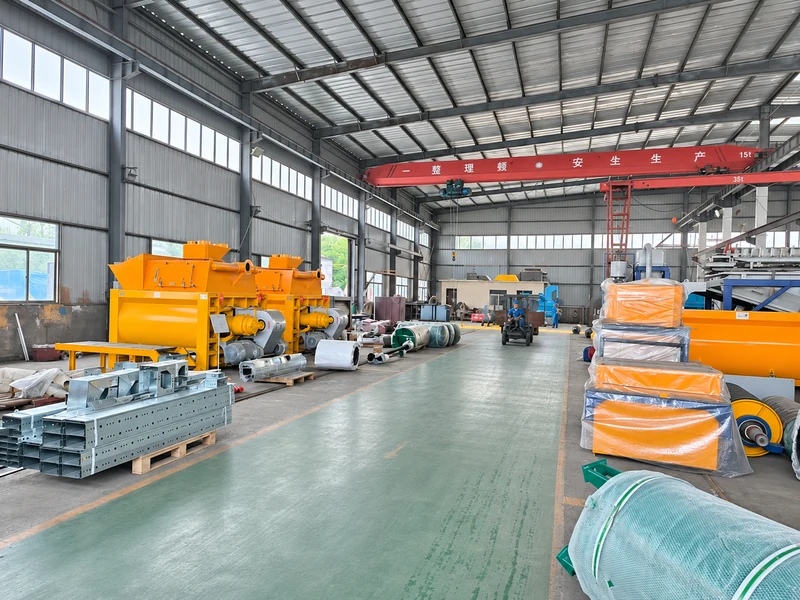
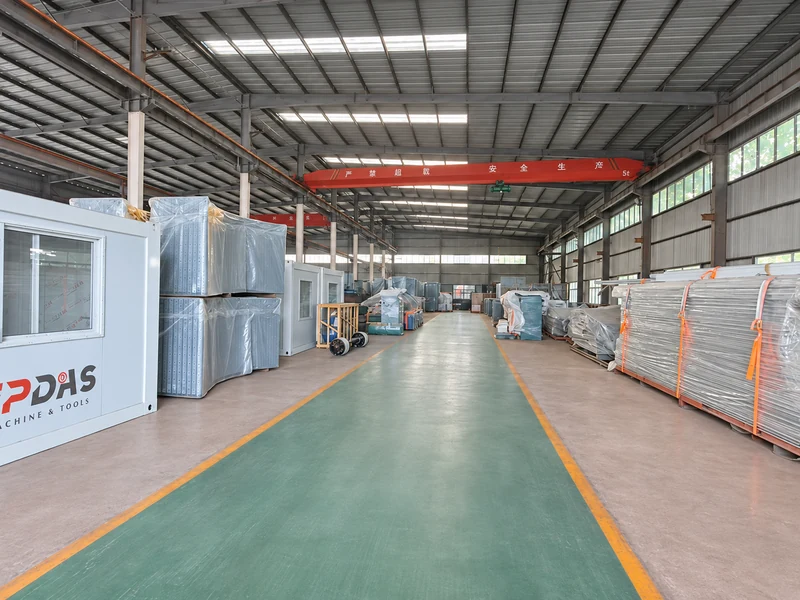
A central-mixing plant coordinates several systems. Their capacities and operating sequences need to work together.
Aggregate Storage and Batching
Aggregate bins separate the sand and stone fractions used in the concrete mix. Their number and storage capacity influence how materials are managed and replenished.
Storage should reflect local delivery patterns as well as production demand. A plant receiving frequent aggregate deliveries may need a different stockyard arrangement from one relying on larger, less frequent shipments.
Keeping materials separated and the loading area organised also helps prevent contamination and unintended changes in grading.
Aggregate Transfer
The transfer system moves weighed aggregate to the mixer. Depending on the selected EPDAS model, this is handled by a hoist bucket or belt conveyor.
Its position affects the relationship between the aggregate bins, mixer structure and vehicle routes. Transfer equipment should be accessible for inspection without creating unnecessary conflicts with loading operations.
JS-Series Mixing Equipment
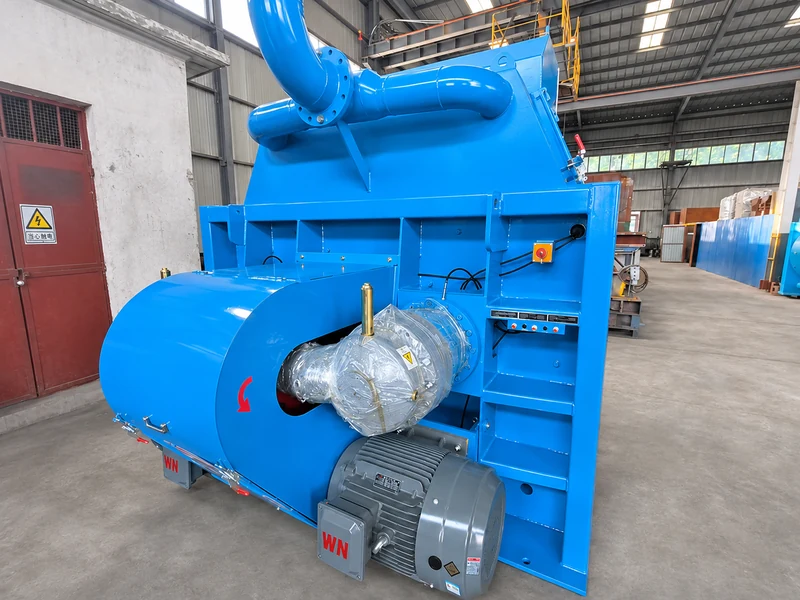
The documented EPDAS model range uses JS-series mixer options, with the mixer specification varying by plant model.
The mixer must suit the intended concrete and production schedule. Batch size, material characteristics and mixing requirements should be reviewed together rather than treating mixer capacity as the only selection criterion.
Water and Admixture Batching
Water and admixtures must be introduced in controlled quantities according to the approved mix design.
The EPDAS specifications include model-related weighing information. During operation, measuring equipment needs appropriate checking and maintenance, while material adjustments should follow the producer’s quality-control procedures.
Cementitious Material Handling
A complete installation also requires suitable arrangements for storing, conveying and batching cementitious materials, together with coordinated equipment controls.
Supply Package and Control Functions
Silo capacity, powder types, conveying equipment and control functions should be defined for the selected supply package. They should not be assumed from the plant model name alone.